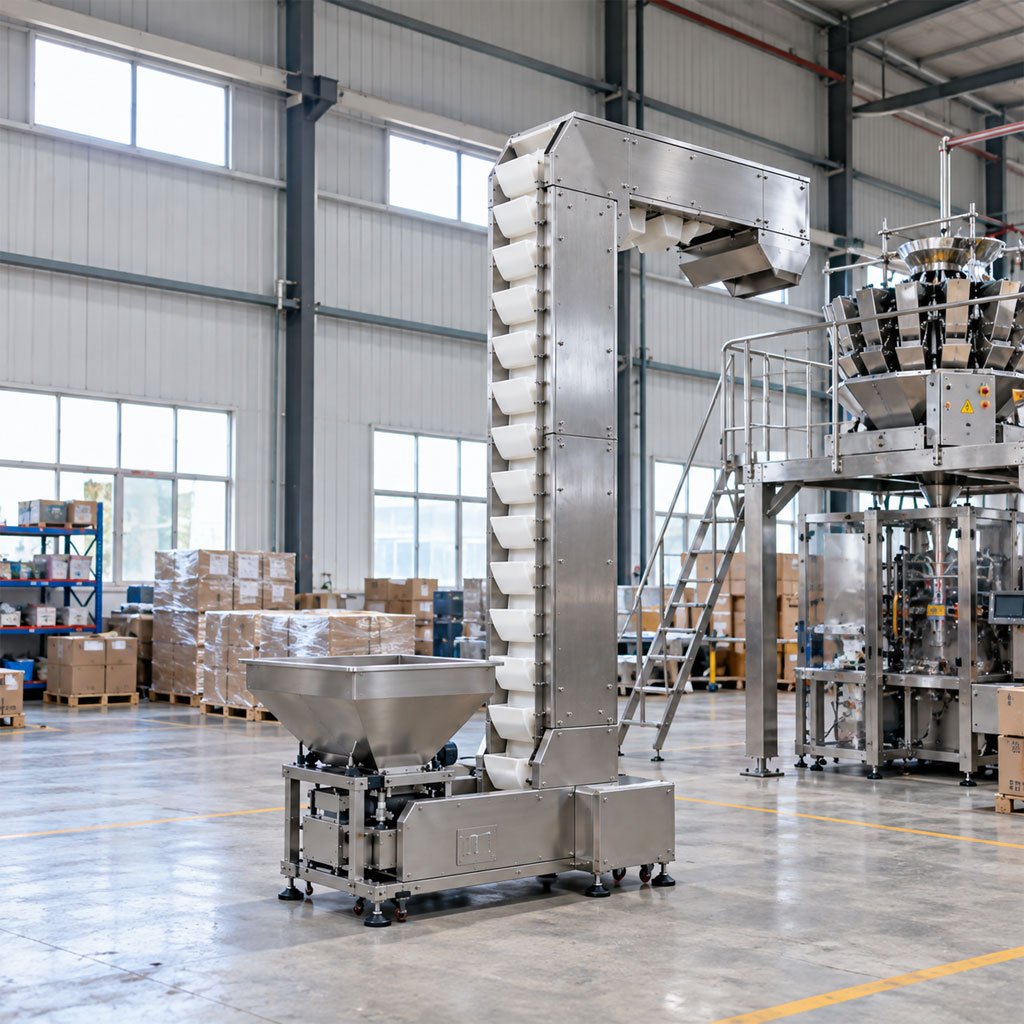
Say Goodbye to High Dust, Inefficient Manual Feeding, and High-Altitude Risks: Experience Vertical, High-Efficiency Conveying and Dust-Free Automated Feeding
Z-type bucket elevators (also known as Z-bucket conveyors or continuous bucket elevators) are essential material handling equipment specifically designed to solve packaging pain points such as difficult vertical and horizontal cross-zone material transport, heavy and hazardous manual high-altitude feeding, dust pollution, product breakage, and complex multi-point discharge interfacing.
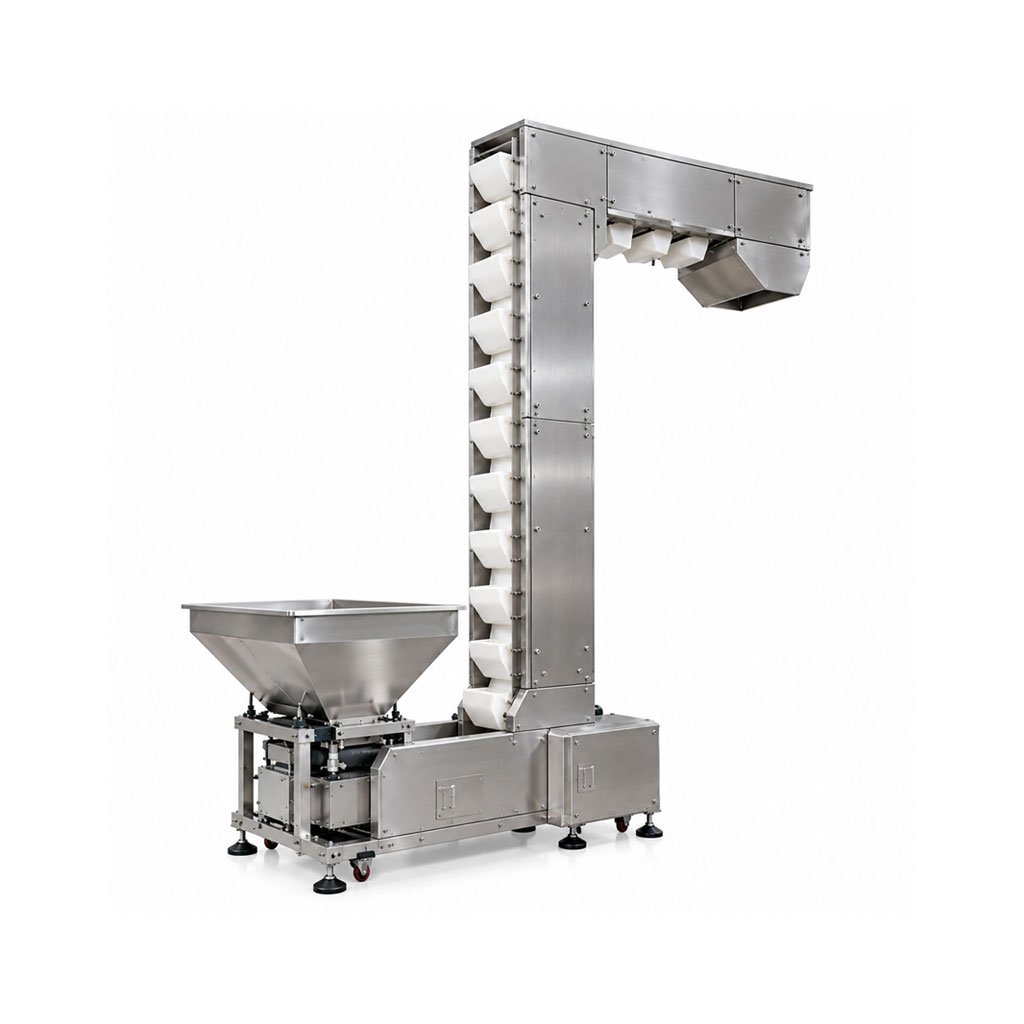
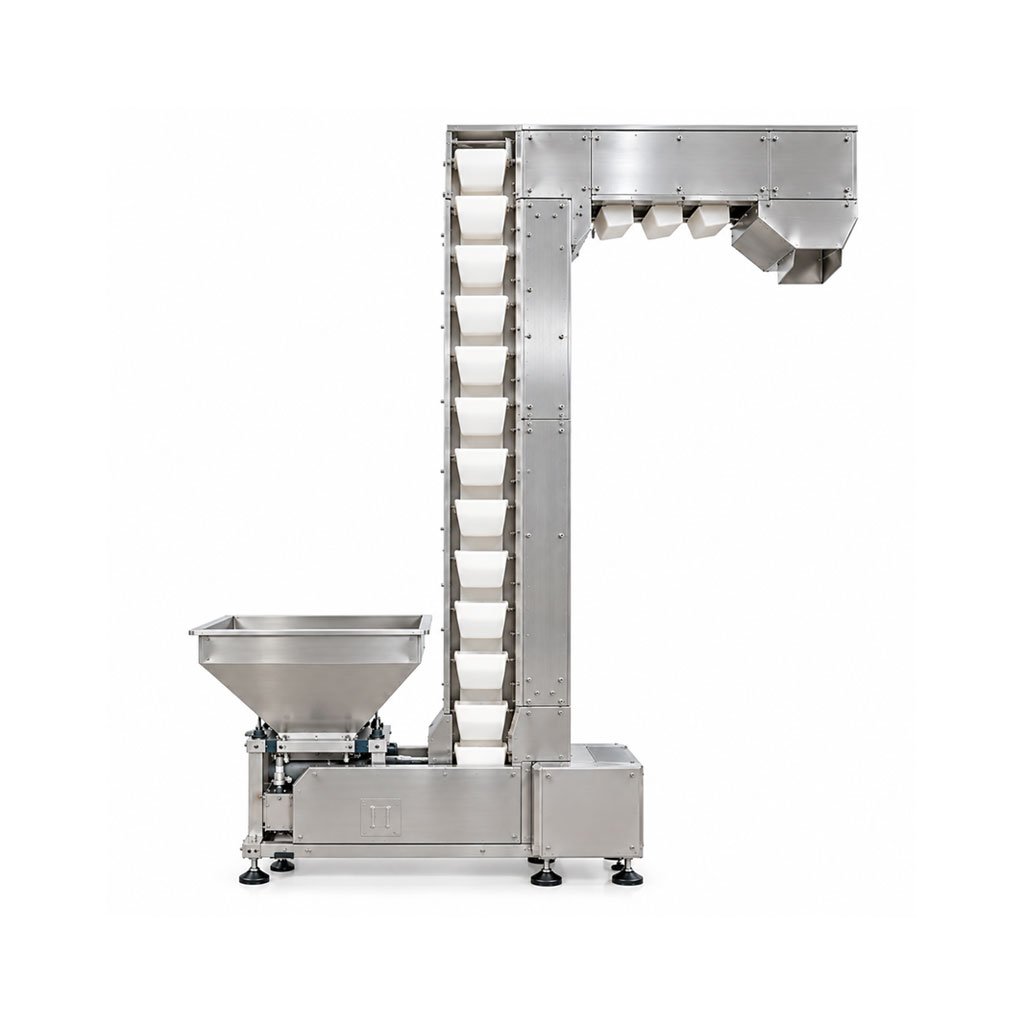
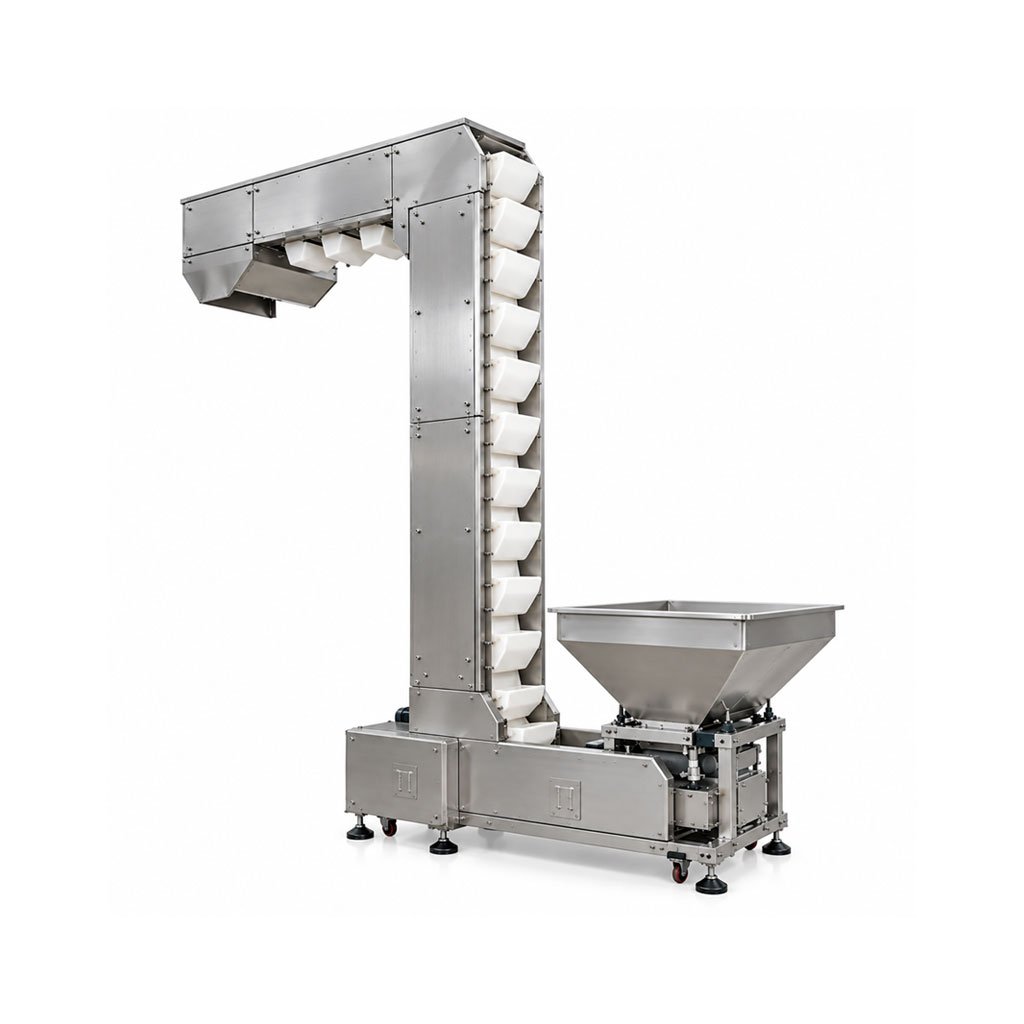
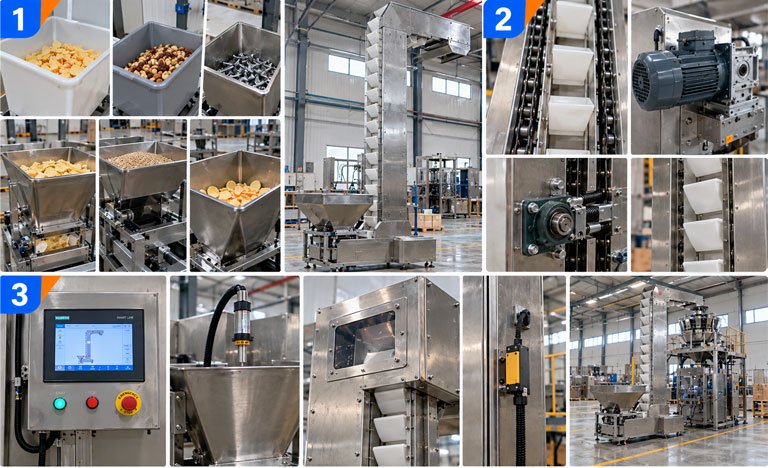
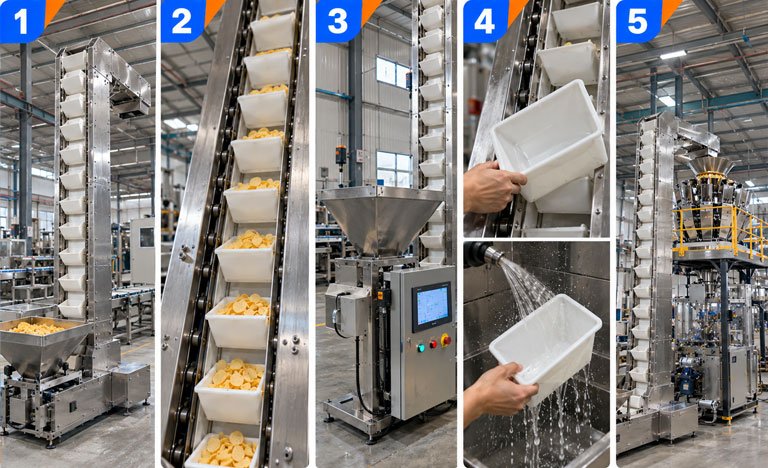
LANTU Machinery introduces a fully customized Z-type bucket conveying and automated feeding solution. Built with a high-strength heavy-duty stainless steel or carbon steel frame, a fully enclosed dust-proof housing, food-grade/industrial-grade plastic (or stainless steel) buckets, and a high-precision chain drive system, it operates across five core automated stations: 1. Automatic quantitative feeding and vibratory loading at the bottom hopper $\rightarrow$ 2. Smooth vertical elevation and horizontal transport along Z-shaped spatial trajectories $\rightarrow$ 3. Smart photoelectric sensing and level-control signal integration $\rightarrow$ 4. Precise bucket tipping and dust-free discharge at target stations $\rightarrow$ 5. Continuous cycle return of empty buckets. Acting as a tireless, gentle, and spill-free vertical conveying expert, it handles puffed food, nuts, plastic granules, pharmaceutical tablets, and chemical powders with ease. The system delivers end-to-end automation—from quantitative loading, lifting, and horizontal transfer to on-demand discharge—ensuring zero product damage, dust-free operation, smooth conveying, and complete independence from manual intervention.
As a source manufacturer of packaging machinery, LANTU Machinery makes the complex automated process—bottom loading, chain driving, Z-bend trajectory tracking, gravity/tipping discharge, and level-linked control—as simple as operating a smartphone. Operators need only select a feeding mode on the central control panel (or link it with upstream/downstream packaging machinery and multihead weighers) and load materials into the bottom storage hopper. The machine automatically transfers materials to high-level equipment (such as multihead weighers, vertical form-fill-seal machines, or reactors) on demand. Achieving conveying capacities of 3–30 cubic meters per hour (customizable for higher volumes), it significantly reduces material handling time while saving labor, time, and costs.
Partnering with a reputable source manufacturer is crucial to maximizing your return on investment. LANTU Machinery combines proven chain-synchronous drive and bucket positioning technology with robust reliability and continuous operational stability to keep your automated lines running smoothly.
Core Components & Three System Guarantees (LANTU Precision Parts)
Our Z-type bucket elevators are equipped with top-tier industrial components to ensure high quality, zero defects, and extended service life.
1.Zero-Damage Feeding & Multi-Material Bucket System
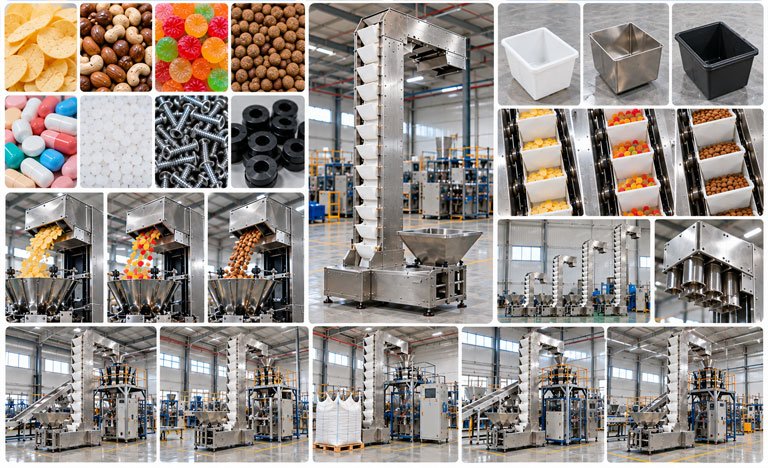
Highly Adaptable Customized Buckets: Food-grade PP (polypropylene), ABS, or SUS304 stainless steel buckets are available. Wear-resistant and temperature-resistant, they comply with FDA/GMP hygiene standards to ensure zero contamination and zero product breakage.
Electromagnetic Vibratory / Screw Feeder: An adjustable vibratory feeding mechanism at the base ensures uniform, continuous loading into passing buckets, eliminating jamming and overflow.
Soft-Landing & Anti-Breakage Design: Optimized loading and discharge angles protect fragile items (such as potato chips, biscuits, and puffed food) via low-drop, gentle conveying.
2.Heavy-Duty Chain & Z-Trajectory Drive System
Dual-Chain High-Strength Synchronous Drive: Wear-resistant alloy steel or low-noise engineering plastic chains paired with precision guide rails ensure smooth, wobble-free bucket travel along vertical and horizontal sections.
VFD Variable-Speed Motor: Industrial VFD motors and reducers allow real-time micro-adjustments of conveying throughput based on downstream packaging machine requirements.
Automatic Tensioning & Anti-Derailment Mechanism: Built-in chain tensioning devices prevent slack, tooth skipping, or derailment during long-term operation.
3.Central Smart Control & Dust-Free Safety Protection System
Siemens / Mitsubishi PLC Control & Level Linking: Industrial-grade PLC controllers interface seamlessly with photoelectric or load sensors on downstream multihead weighers and packaging hoppers, enabling automatic startup when low on material and automatic stop when full.
Fully Enclosed Dust Cover & Inspection Windows: The enclosed structure (with optional clear acrylic inspection windows) prevents dust leakage, keeping workshops clean.
Overload, Jam, & Chain-Break Protection: Smart sensors detect resistance anomalies in real time, triggering millisecond-level emergency stops during obstructions to protect motors and mechanical structures.
Specifications and Technical Parameters
| Technical Parameter Item | LT-ZC-160 (Standard 1.6L High-Speed Z-Bucket Elevator) | LT-ZC-400 (Large Capacity 4.0L/6.0L Heavy-Duty Z-Bucket Elevator) |
| Conveying Capacity | Depends on material bulk density and speed | Supports large-batch, heavy-duty continuous feeding |
| Bucket Volume & Material | 1.6L (Food-grade PP / ABS / SUS304 stainless steel) | 4.0L / 6.0L (Thickened food-grade PP / SUS304 stainless steel) |
| Lifting Height & Horizontal Span | Lifting height: 2.0–6.0 m / Horizontal section: 1.5–5.0 m (Customizable) | Lifting height: 3.0–12.0 m / Horizontal section: 2.0–10.0 m (Customizable) |
| Material Damage Rate | Near 0% (Static loading with no squeezing or collision) | Near 0% (Low drop design optimized for fragile products) |
| Feeding Method | Electromagnetic feeder (Stepless fine adjustment of flow rate, with bottom storage hopper) | Heavy-duty electromagnetic / belt / screw quantitative feeder (Can be equipped with large-capacity storage bin) |
| Discharge Method | Single-point top tipping discharge (Optional pneumatic multi-point discharge unit) | Single-point / pneumatic multi-point selective tipping discharge (One-to-many supply) |
| Drive & Transmission System | Gear reducer motor + Inverter + High-strength double-strand alloy steel chain | Heavy-duty gear motor + Stepless inverter + Wear-resistant engineering plastic/steel chain |
| Conveying Belt / Chain Speed | 0 – 25 m/min (Stepless frequency variable speed control) | 0 – 20 m/min (High torque, smooth operation) |
| Operation & Control System | Siemens/Mitsubishi PLC + HMI Touchscreen (With material level sensor linkage) | Industrial-grade PLC + Touchscreen (Supports multi-line material level intelligent scheduling) |
| Casing & Dustproof Structure | SUS304 Stainless Steel / Carbon Steel Spray-coated fully enclosed dust cover | SUS304 Stainless Steel full enclosure / Optional transparent acrylic observation window |
| Air Supply Requirement (For Multi-point Discharge) | 0.4 – 0.6 MPa ($\ge 0.15\text{ m}^3\text{/min}$) | 0.4 – 0.6 MPa ($\ge 0.25\text{ m}^3\text{/min}$) |
| Power Supply & Total Power | AC 220V/380V / 50Hz / 0.75–1.5 kW | AC 380V / 50Hz / 2.2–4.0 kW |
| Safety & Protection Functions | Automatic chain tensioning, millisecond-level stop on bucket jamming, overload/material shortage alarm | Chain breakage protection, foreign object jamming sensor stop, anti-overload audible and visual alarm |
| Integrable Expansion Lines | Multi-head combination weighers, vertical packaging machines, premade pouch packaging machines, checkweighers | Large dosing bins, multi-line distribution systems, vertical packaging machines, automated storage systems |
Note: Actual conveying capacity depends on material flowability, bulk density, and hopper fill rate. Lantu Machinery offers custom layouts—such as Z-type, C-type, or Z-T combined configurations—tailored to the client’s facility space (including ceiling height) and the heights of upstream and downstream equipment.
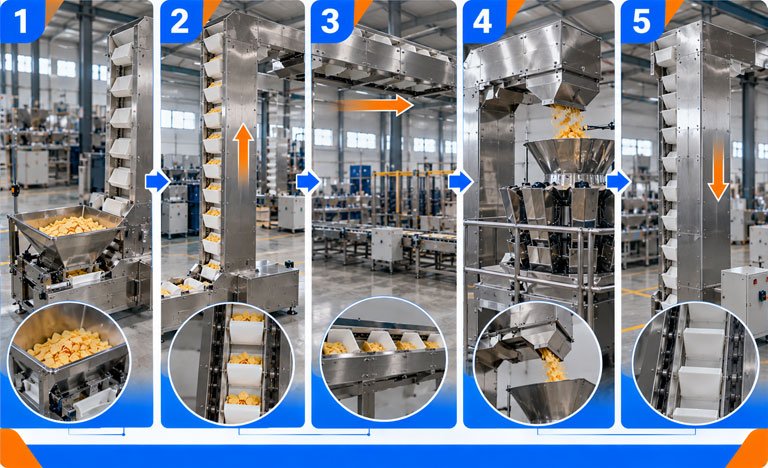
Step-by-Step Z-Type Bucket Elevator Workflow
Station 1 (Material Loading & Quantitative Feeding): Bulk material is loaded into the bottom hopper, where the vibratory feeder feeds it evenly into circulating buckets below.
Station 2 (Horizontal Entry & Vertical Elevation): Filled buckets move along horizontal rails driven by the chain assembly before transitioning smoothly into vertical ascent.
Station 3 (High-Level Horizontal Conveying & Obstacle Crossing): Upon reaching the target height, buckets transition into the upper horizontal segment, traversing machinery and aisle obstacles.
Station 4 (Bucket Tipping & Precise Discharge): Upon reaching designated discharge stations (available in single or multi-point configurations), buckets tip or rotate to pour material into target hoppers.
Station 5 (Empty Bucket Return & Continuous Cycle): Emptied buckets return to their upright orientation and travel along the return track back to the bottom feeding zone for continuous operation.
Applicable Material Specifications & Industry Guidelines
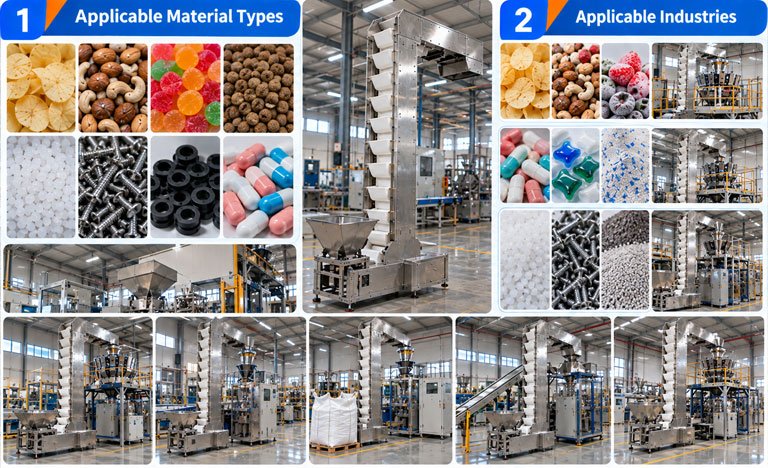
Designed for maximum operational efficiency, LANTU Machinery’s Z-type bucket elevator features exceptional compatibility across diverse industries and material types:
1.Applicable Material Formats
Granular & Bulk Items: Candies, nuts, snacks, puffed food, pet food, frozen food, etc.
Powder-Granule Mixes & Small Components: Plastic pellets, chemical raw materials, hardware fasteners, small rubber parts, pharmaceutical tablets/capsules, etc.
Capacity Capabilities: Elevation heights from 2–12m, horizontal spans from 1.5–10m (fully customizable), with bucket capacity options of 1.6L, 4L, or 6L.
2.Target Industries
Food, Snack & Frozen Products: Feeding multihead weighers, vertical packaging machines, puffed food lines, and nut packaging systems.
Pharmaceuticals, Personal Care & Daily Chemicals: Pre-bottling tablet/capsule feeding, laundry pod/tablet handling, and cosmetic part supply lines.
Plastics, Chemicals & Hardware: Injection molding machine feeding, resin pellet elevation, and hardware screw packaging supply.
5 Reasons to Choose LANTU Machinery Z-Type Bucket Elevators
High operational stability, low product breakage, and easy sanitization are essential when investing in automated material handling equipment. LANTU Machinery delivers plug-and-play, durable performance in every build.
Z-Type Spatial Conveying Saves Floor Space: Combines horizontal and vertical movement into a compact footprint that easily navigates over existing machinery and walkways.
Zero Product Damage Preserves Quality: Buckets remain upright throughout travel and tip only at discharge points, drastically minimizing particle collisions and friction.
Smart Level Linking for Unattended Feeding: Communicates seamlessly with downstream packaging machines or multihead weighers, starting and stopping automatically based on demand.
Easy-Clean Design Meets Hygienic Standards: Buckets and dust covers feature quick-disassembly structures with no sanitary dead zones, facilitating fast washdowns and product changeovers.
Factory Material Testing Before Delivery: Every unit undergoes rigorous endurance and load testing with real materials (heavy, fragile, or granular) prior to shipment to ensure zero bucket jamming or vibration faults.
Key Factors to Consider When Purchasing a Z-Type Bucket Elevator
Consider these primary indicators to select the right system for your facility:
Material Properties & Bucket Material Selection:
Food / Pharmaceutical / Corrosive Goods: Opt for food-grade PP buckets or SUS304 stainless steel buckets.
Heavy-Duty / Hardware / High-Abrasive Items: Opt for reinforced impact-resistant ABS or carbon steel buckets.
Required Throughput ($m^3/h$ or Tons/Hour):
1.5–5 $m^3/h$: Standard 1.6L buckets (ideal for small-granule, high-precision packaging lines).
6–15 $m^3/h$: Medium 4L buckets (ideal for standard food packaging lines).
15–30+ $m^3/h$: Heavy-duty 6L+ buckets (ideal for bulk, high-capacity production lines).
Dimensional Constraints (Lifting Height & Horizontal Span): Confirm ceiling height, bottom loading height, and target discharge clearance (e.g., 10-head or 14-head multihead weighers).
Discharge Point Requirements: Single-point discharge (servicing one packaging machine) or multi-point pneumatic discharge (servicing multiple hoppers or packaging lines).
Line Integration Needs: Check compatibility with upstream vibratory feeders/tippers and downstream multihead weighers, VFFS machines, or premade pouch packing machinery.
Frequently Asked Questions (FAQ)
Q1: Will the machine crush or abrade fragile materials (such as potato chips, rock sugar, or rice crackers)?
Answer: No. Z-type bucket elevators utilize a bucket-carrying principle where materials remain stationary inside individual buckets as they travel. Because there is no relative friction or squeezing, and because loading drops are kept minimal via vibratory feeding, product breakage is reduced to near 0%.
Q2: Can a single Z-type elevator feed multiple packaging machines simultaneously?
Answer: Yes. LANTU Machinery offers customizable multi-point discharge Z-type elevators. Pneumatic tipping mechanisms along the upper horizontal section open dynamically based on level signals from downstream machines, ensuring precise, on-demand distribution.
Q3: Can this elevator integrate seamlessly with multihead weighers and vertical form-fill-seal machines?
Answer: Yes. All LANTU Machinery handling systems feature modular hardware and standard industrial PLCs (supporting digital signals, RS485, and dry contacts) for effortless integration with multihead weighers, premade pouch machines, flow wrappers, and checkweighers into a fully automated line.
Contact the Source Manufacturer Today for Your Custom Z-Type Bucket Elevator Solution!
LANTU Machinery — Specialized Packaging Equipment Manufacturer with Factory-Direct Quality.